Bogie Hearth Furnace Technology Redefining Industrial Thermal Processing
2026-10-13
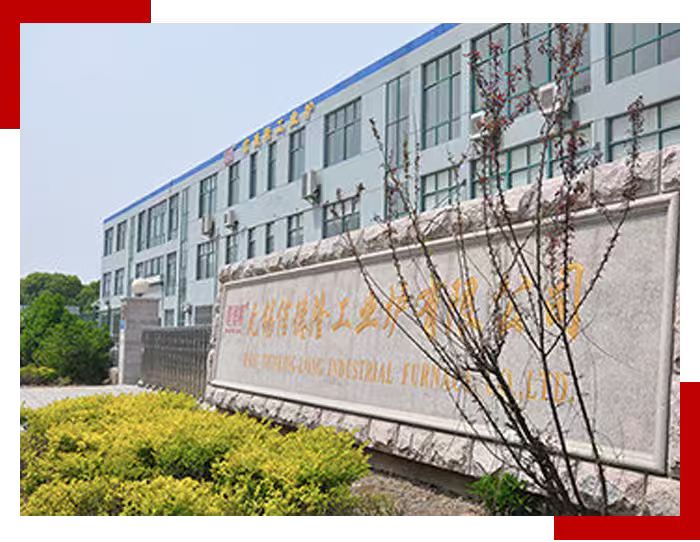
Industrial thermal processing hasn't seen a genuine leap forward in decades—until now. Bogie hearth furnace technology is quietly rewriting the rules, offering precision and efficiency that legacy systems simply can't match. From heavy fabrication to advanced ceramics, the shift isn't incremental; it's structural. As facility managers chase tighter tolerances and lower energy costs, this innovation demands attention. At the forefront, THINKING-LONG is turning what was once a constraint into a competitive edge. Here's why the next era of heat treatment will be defined by those who embrace the bogie hearth difference.
Not All Furnaces Are Built for the Long Haul
A furnace’s lifespan often comes down to details that never make the brochure. Cheap heat exchangers develop hairline cracks after a few seasons, while thin cabinet panels rust from basement moisture or coastal air. The difference isn’t always obvious on day one—it shows up three winters later, when the repair bill lands. Builders who specify long-haul units look for heavier gauge steel, sealed burner compartments, and components that don’t rely on plastic clips to hold critical parts together.
Ignition systems tell a quieter story. Entry-level models frequently use single-stage gas valves that cycle hard and fast, stressing every joint and seal. Mid-tier and premium furnaces often feature modulating burners or at least two-stage firing, which reduces thermal shock and keeps the blower from slamming on and off. Over a decade, that gentler cycling means fewer solder joints fail, fewer circuit boards fry, and far less dust gets baked onto the heat exchanger.
Then there’s serviceability. Some furnaces force a technician to remove a dozen screws and a wiring harness just to inspect the flame sensor. Others have tool-less access panels and clearly labeled test points. Long-haul designs plan for maintenance instead of treating it as an afterthought—because a furnace that’s easy to clean and check is a furnace that actually gets cleaned and checked. That alone can add five or ten years to its working life.
Where Temperature Uniformity Stops Being a Buzzword
The spec sheet can list a number for temperature uniformity, but real performance shows up when a batch of materials comes out with consistent properties from edge to center. That’s the point where uniformity stops being a marketing term and starts to matter for repeatable results.
In many thermal processes, a few degrees of drift between zones can ruin a whole run. Equipment that maintains tight uniformity under load, not just in an empty chamber, gives operators confidence to push cycle times without sacrificing quality.
Checking uniformity means placing multiple probes at different positions and depths, often with a typical production load inside. If the readings stay within a narrow band across the entire working volume, then the claim has actual weight behind it.
Loading and Unloading Without the Bottleneck
Warehouse docks often hum with activity, yet the real constraint isn't the volume of pallets—it's the waiting. Trucks queue for a bay, forklifts circle for a clear path, and hand-offs stall when paperwork outpaces the physical move. The first step to unloading without a bottleneck is to treat the dock as a synchronized system, not a series of isolated tasks. Staging zones placed just inside the door, with pre-assigned drop points for each incoming shipment, let workers offload directly onto designated carts instead of stacking randomly and sorting later. This small shift removes the stop-start rhythm that drains hours from every shift.
Another overlooked friction point is the mismatch between arrival schedules and staffing. A rigid eight-hour window invites a morning surge and an afternoon lull, forcing crews to sprint and then idle. Instead, stagger dock appointments using live data from carriers—adjusting slot times in fifteen-minute increments based on actual traffic, not a printed manifest. Pair this with cross-trained team members who can switch between unloading, sorting, and replenishment as the flow dictates. The goal isn't faster lifting; it's eliminating the pauses where nothing moves and nobody knows why.
Equipment choice also quietly shapes throughput. Standard pallet jacks force workers to travel long, empty return paths, while a simple gravity roller section near the dock edge lets boxes glide inward with minimal walking. For mixed loads, consider modular carts with removable shelves that roll straight from trailer to aisle, bypassing the traditional staging pile entirely. When every motion has a purpose and every hand-off happens at the point of use, loading and unloading stops being a chokepoint and becomes just another steady beat in the warehouse rhythm.
Energy Consumption: The Overlooked Variable in Thermal Processing
In most heat-treating shops, energy is treated as a fixed overhead cost—something to be negotiated with the utility company, not a variable that can be tuned like furnace temperature or quench severity. Yet two identical loads of the same alloy, run through the same furnace on different days, can show a 20% swing in energy consumption simply because of how the baskets were stacked, how long the door was open during transfer, or whether the burners were tuned for the last campaign. This variability rarely appears on the shop floor dashboard, and when it does, it is often dismissed as noise. The truth is that energy is one of the few process inputs that can be reduced without altering the chemistry or mechanical properties of the parts, yet it goes unmeasured in many facilities.
Bringing energy into the conversation as a controllable process variable changes how engineers approach cycle design. For example, many heat treatments still use conservative ramp rates and extended soak times because those recipes were validated decades ago when fuel was cheap and sensors were less reliable. By re-evaluating these parameters with modern thermocouples and data logging, it is often possible to trim both peak power demand and total kilowatt-hours per kilogram of parts. Adjustments such as reducing empty furnace idling, improving door seals, or recovering heat from exhaust gases can yield double-digit percentage savings without risking metallurgical quality. These are not exotic technologies; they are operational choices that get ignored precisely because energy consumption is not treated with the same rigor as temperature uniformity or hardness.
The reluctance to monitor energy also ignores the growing pressure from customers and regulators to disclose carbon footprints. Even if a shop does not face immediate fines, the cost of wasted kilowatt-hours will eventually surface in profit margins or equipment maintenance. Treating energy as an overlooked variable does not require a complete overhaul of the heat-treating line; it starts with metering individual furnaces, setting baseline energy intensities, and challenging long-standing practices that were never optimized for efficiency. Once operators see how much variation exists between shifts or loads, they begin to ask the right questions—why is furnace three using more gas than furnace two, and what can be done about it before the next energy audit brings bad news.
From Castings to Forgings: A Thermal Workhorse in Action
The shift from castings to forgings isn't just a materials swap—it's a complete rethink of how a component handles thermal stress, fatigue, and the punishing cycles of real-world operation. Cast parts, with their inherent porosity and less predictable grain flow, often hit their ceiling when temperatures swing hard or loads spike repeatedly. Forgings, by contrast, come out of the die with a continuous, aligned grain structure that follows the part's geometry. That alignment is the quiet hero: it channels heat away from critical zones, resists crack initiation, and shrugs off the thermal ratcheting that would send a casting to early retirement.
In service, a forged thermal workhorse rarely gets a break. Think of exhaust manifolds, turbine housings, or high-pressure valve bodies—components that live between ambient chill and several hundred degrees, multiple times a day. Where a casting might develop micro-fissures at grain boundaries or hot spots from uneven density, a forging spreads the thermal load more evenly. The result isn't just longevity on paper; it's fewer unplanned teardowns, tighter clearances maintained over time, and a part that can be pushed closer to its metallurgical limits without the nagging worry of hidden voids.
But making that leap from casting to forging requires more than a drawing change. Tooling must be designed for metal flow, not just shape replication. Process engineers have to rethink cooling channels, fillet radii, and even the starting billet temperature. It's a collaboration between design intent and forgeability—one that, done right, turns a thermal workhorse into the kind of component that operators forget about because it simply keeps working.
Why Maintenance Teams Keep Requesting Bogie Hearth Configurations
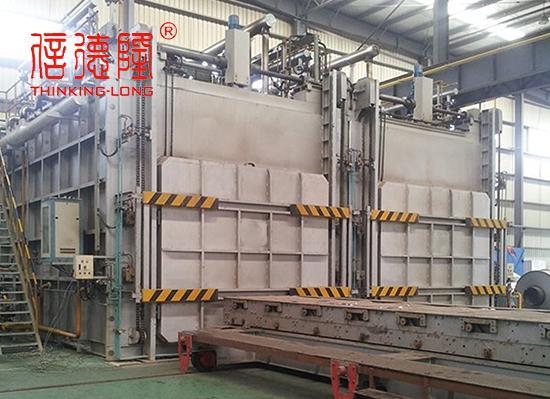
For a lot of maintenance crews, the appeal of a bogie hearth setup comes down to access. When the entire hearth rolls out of the furnace, inspection and repair work no longer has to be done in a cramped, hot box. Crews can walk around the load, check burners and seals from a comfortable position, and replace refractory sections without setting up temporary scaffolding inside the chamber. That alone cuts hours off typical preventive maintenance routines.
Loading practices also play a role. Because the hearth can be loaded outside the furnace, the crew can stage the next batch while the current cycle is still running. The door stays open for a much shorter time, which reduces thermal shock to the lining and keeps temperature swings from creating cracks. Fewer cracks mean fewer unplanned repairs and less time chasing air leaks.
There is also the matter of spare parts. A bogie hearth is essentially a movable platform with its own wheels, drives, and seals. Many of these components can be rebuilt offline or swapped as an assembly. Maintenance teams can prepare a fully refurbished hearth car while the furnace is still in production, then roll it into place during a scheduled shutdown. That kind of predictability is rare with fixed-hearth designs.
FAQ
Unlike fixed-chamber batch units, a bogie hearth furnace uses a wheeled, rail-mounted car that rolls out completely for loading. This eliminates crane reach limitations and allows entire assemblies to be staged outside the heated zone. The result is faster turnaround, safer material handling, and less risk of thermal shock to refractory linings.
The movable hearth essentially doubles as a transport platform. Operators can pre-load massive components, heat exchanger bundles, or stacked castings on a spare car while another load is still soaking. Once the cycle ends, the first car rolls out and the second rolls in within minutes, slashing idle time between batches.
Heavy fabrications, pressure vessels, and large casting sets are prime candidates. The technology really shines where parts are too bulky or awkward for fork trucks inside a conventional chamber. Stress relieving after welding, full annealing of large forgings, and even certain hardening cycles for wind turbine components are common.
Yes, provided the burner and airflow arrangement is designed correctly. A well-engineered bogie hearth furnace uses multiple high-velocity burners and recirculation fans to maintain temperature uniformity within a 10-degree Celsius band across the load. This is critical for stress relieving where uneven heating can reintroduce residual stresses rather than remove them.
Modern PLC and SCADA systems allow ramp-soak programming tied to thermocouple feedback from the load itself, not just the chamber. Adaptive tuning adjusts burner firing rates in real time to follow the ideal heating curve, which reduces distortion and energy waste. It has moved from simple on-off control to true process management.
Common approaches include refractory fiber linings instead of dense brick, regenerative burners that preheat combustion air with exhaust heat, and tight sealing around the bogie perimeter. Some facilities also recover waste heat for plant heating or preheating incoming loads. Payback can be under three years for high-utilization units.
The rail system and bogie wheels require regular inspection because they carry enormous weight and see thermal cycling. Also, the sand seal or ceramic fiber seal between the car deck and furnace shell needs periodic replacement to prevent hot gas leakage. Ignoring these simple items leads to uneven heating and higher fuel costs.
Conclusion
Most industrial furnaces struggle when cycles get heavy and loads vary widely, but bogie hearth designs ignore that pattern. The movable hearth car eliminates the usual bottleneck of charging and discharging; operators can stage a fully loaded car outside the chamber, roll it in, and pull it out just as smoothly. That fundamentally changes how temperature uniformity is achieved—because the car forms part of the heating chamber, workpieces aren't shoved through narrow doors or crammed against hot spots. In practice, this means castings and forgings come out with consistent metallurgical properties batch after batch, not just within a single test coupon. The structure also handles repeated thermal expansion without warping the refractory, which is why these furnaces last longer in demanding heat-treat shops.
Energy consumption is where bogie hearths quietly outperform expectations. Instead of losing heat each time a door opens, the roll-out hearth lets crews load and unload quickly, cutting idle time and fuel waste. Maintenance teams tend to request these configurations because the floor-level access reduces crane dependency and simplifies inspection of burners, seals, and hearth wheels. A furnace that spends less time cooling down between cycles and less effort fighting misaligned doors is simply cheaper to run. When you combine that with the range of parts—large castings, heavy forgings, weldments—the bogie hearth becomes less of a specialty tool and more of a standard for plants that cannot afford downtime or uneven heating.
Contact Us
Contact Person: Qian Xijun
Email: [email protected]
Tel/WhatsApp: 8613961736750
Website: https://www.thinkinglong.com/